
Project estimating
Quick answer
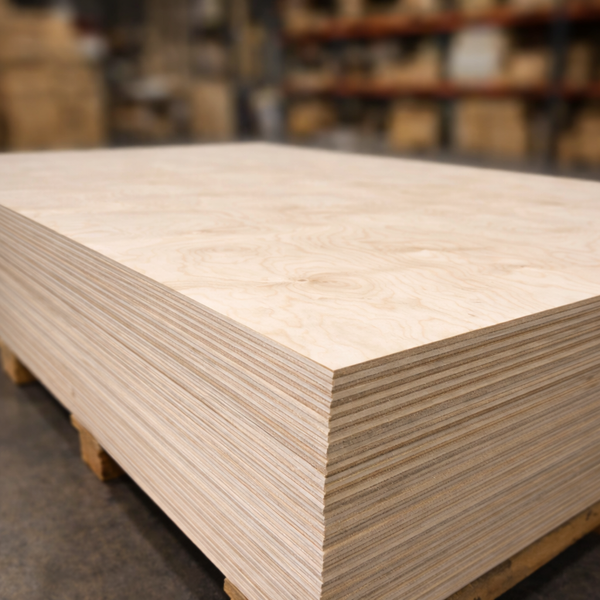
The cost of 4×8 plywood is not just the shelf price of one sheet. A useful estimate includes the number of sheets your cut layout actually consumes, cutting waste, finishing labor and materials, edge treatment, handling and delivery. The lowest-priced sheet can produce the higher finished-part cost if it creates more waste or shop work.
Use current product-page pricing only after the panel specification is fixed. Then calculate yield from the real sheet size, grain direction and kerf. Add process costs that differ between raw, clear prefinished and decorative-surface panels.
The complete equation
A plywood cost formula that reflects shop reality
Sheets
Required sheet count × current price for the exact thickness, face, core and finish.
Waste
Material left after nesting, kerf, defects, grain matching and reserve parts.
Process
Shop labor and supplies for sanding, coating, edge treatment, masking and touch-up.
Logistics
Delivery, unloading, storage, protection and moving full sheets through the shop.
Berta’s plywood cut-list calculator is the right starting point because parts—not square footage—drive sheet count. Use the sheet-material calculator as a broader quantity check and the plywood pallet calculator when order size affects handling plans.
Cost categories
What belongs in a 4×8 plywood estimate
| Cost category | How to calculate it | Common omission | Best evidence |
|---|---|---|---|
| Panel purchase | Current exact-variant price × planned sheets | Comparing unlike cores, grades or finishes | Live product page and written specification |
| Cutting waste | Sheets purchased minus usable parts and approved reusable remnants | Assuming every remaining square foot is reusable | Nest drawing with kerf and grain direction |
| Finish materials | Primer/sealer/topcoat, abrasives, applicators and cleanup supplies | Coating both sides and edges | Test-panel coverage and coating-system data |
| Finish labor | Preparation + application + between-coat work + handling | Counting cure time as free when it blocks racks or schedule | Shop labor standard or timed sample |
| Edge treatment | Visible edge length × material plus setup and trimming | Inside edges, shelves and repair allowance | Edge schedule linked to cut list |
| Machining | Cutting, drilling, CNC time and tooling allowance | Extra handling for delicate finished faces | Machine rate and proven cycle time |
| Delivery and unloading | Current quote plus required people/equipment | Access limits, lift-gate or indoor carry requirements | Confirmed order details and site plan |
| Risk reserve | Project-specific allowance for replacement parts or visual matching | Using one percentage for every project | Prototype, material consistency and complexity |
Yield before price
Why the cut map can change the “cheapest” sheet
A 4×8 sheet contains 32 nominal square feet, but cabinet parts rarely consume it with perfect efficiency. Grain direction may prevent rotating parts. A finished face may require all show parts to run consistently. Saw kerf removes material at every cut, and a narrow leftover can be too small for the next cabinet.
The plywood kerf and cutting-allowance article explains why a layout drawn with zero-width cut lines overstates yield. The plywood sheet-size reference also matters: “4×8” may be used as a familiar category label, while listed metric dimensions and actual sheet dimensions govern fit.
Simple estimating example
A project needs ten long cabinet sides plus shelves and stretchers. Area alone suggests three sheets. Once the long grain direction, kerf and part spacing are applied, the sides may occupy most of three sheets and push shelves onto a fourth. The correct material budget is four sheets before reserve—not three sheets plus an unexplained overrun.
Rule: do not round the sheet count until after nesting. Round up the final sheet result, then decide whether a project-specific spare is justified.
Raw versus factory-finished
Compare completed surfaces, not only panels
| Workflow item | Unfinished plywood | Factory-finished plywood | Cost question |
|---|---|---|---|
| Surface preparation | Inspect, sand and clean for the chosen coating | Protect the finished face and prepare only where required | How many shop hours does the batch require? |
| Coating | Finish materials, application and cure schedule | Factory surface already present; edges may still need treatment | Does the factory finish meet the design? |
| Color control | Shop controls the system but also owns sample approval and variation | Current panel sample sets the baseline | Will sheets be grouped for visible adjacency? |
| Assembly | Raw faces may accept the intended glue after normal preparation | Bonding areas may need model-specific surface preparation | Has the adhesive joint been tested? |
| Repair | Touch-up can be integrated with the finish schedule | Repairs must match the factory surface | What is the approved repair route? |
If a factory surface removes coating labor and schedule risk, a higher sheet price may lower the cost per installed cabinet. If the project needs a custom stain or painted system, raw plywood may be the correct economic choice. Berta’s Baltic Birch cost article gives a species-specific view; this framework applies across plywood types.
Estimating workflow
Build a quote in six passes
1. Freeze the specification
Name the product, thickness, face, core, finish, sheet size and required documentation. Do not compare a raw panel with a finished panel as if they are identical inputs.
2. Nest the parts
Include grain direction, kerf, margins and visible-face orientation. Separate parts that can use remnants from those needing full-length stock.
3. Add an evidence-based reserve
Base spare material on visual matching, complexity, site risk and replacement lead time—not an automatic percentage.
4. Price shop operations
Add sanding, finishing, edge work, CNC or saw time, masking, handling and repairs using actual shop rates.
5. Plan movement
Use the plywood weight-planning article and delivery and unloading checklist to define labor and equipment.
6. Compare completed-part cost
Divide total material-and-process cost by approved usable parts. Keep sheet price visible, but do not let it stand in for the whole decision.
Current material directions
Price the exact panel after choosing the workflow
No price is embedded here because product pricing changes. The linked product page is the correct place to confirm the current amount at review time.

Unfinished BB/BB Baltic Birch
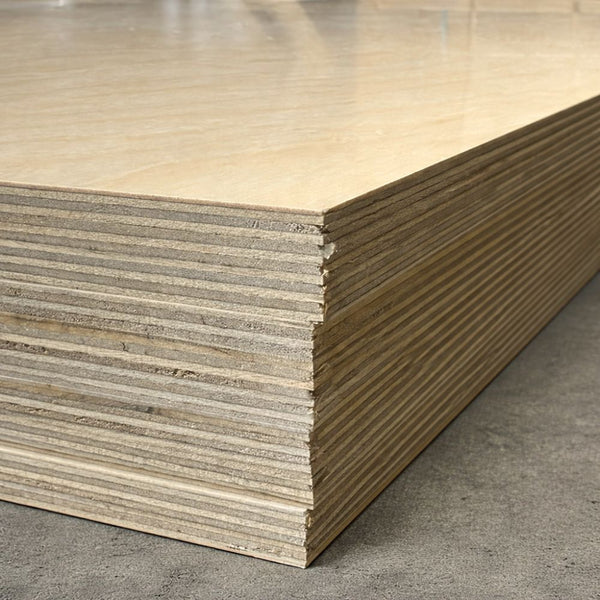
Use this cost path when the project values a solid-birch multi-ply core and shop-controlled finish. The current 3/4-inch listing specifies 18 mm, 4×8, 13 plies and unfinished BB/BB faces.
Add: finish supplies, labor, cure capacity and edge work.
Check current BB/BB specifications
3/4-inch prefinished Birch
Use this comparison when a light birch face and factory-applied UV clear finish on both sides meet the design. The current listing specifies 18 mm, 48×96 inches, Grade A face and multi-ply poplar core.
Add: finished-face protection, edge treatment and any special bonding preparation.
Check current prefinished Birch details
3/4-inch prefinished Maple
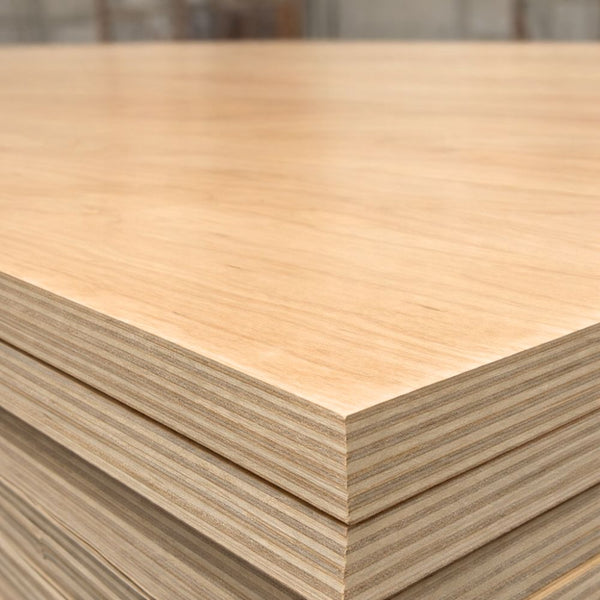
Price maple separately when its appearance is specified. The current Berta variant is listed as 18 mm, 48×96 inches, clear UV finished on both sides with an A-grade maple appearance veneer and 11-ply hardwood construction.
Add: visual matching, edge treatment and protection through installation.
Check current prefinished Maple detailsBrowse the complete plywood collection, narrow the core options in the Baltic Birch collection, or compare workflow-ready surfaces in the prefinished plywood collection. Then use the delivery estimator with the final sheet count.
Frequently asked questions
Plywood cost FAQ
How much does a 4×8 sheet of plywood cost?
There is no single durable answer because thickness, face species, grade, core, finish and market timing differ. Confirm the current price for the exact product, then calculate how many sheets the cut layout consumes.
How do I estimate plywood waste?
Nest the real parts inside the listed sheet dimensions with grain direction, kerf and margins. Treat only reusable remnants as recovered value. The difference between purchased sheets and usable output is the material-waste portion.
Is prefinished plywood cheaper than unfinished plywood?
It can be cheaper per completed part when the factory finish replaces enough sanding, coating and curing labor. Unfinished plywood can be more economical when the project requires a custom finish or when shop finishing is already efficient.
Should I compare plywood by square-foot price?
Square-foot price is a rough material comparison, not a project estimate. Part geometry, grain direction, surface quality, finishing and edge work determine the actual cost per usable component.
How much extra plywood should I order?
Use a project-specific reserve based on nesting efficiency, defect tolerance, appearance matching, complexity and the cost of remaking a damaged part. A fixed percentage is convenient but not equally defensible for every job.
Make cost follow the cut list
Start with the material specification, convert the parts into a real nest, and add the labor and logistics that change with the panel. That process turns “plywood cost” from a shelf-price question into a usable project budget—and makes raw, prefinished and decorative panels comparable on the same finished-part basis.
Scope: Berta product specifications and URLs were checked on October 10, 2026. Prices are intentionally omitted because they can change; confirm current pricing on each product page. Yield examples are planning illustrations, not guarantees. Measure the actual panel and use current coating, hardware and delivery instructions for the exact project.