
Berta Store · Finished-panel joinery
Quick answer
You can assemble prefinished plywood with glued joints, but the adhesive must suit the actual surfaces touching inside each joint. A raw plywood edge meeting exposed wood is a different bond from a raw edge meeting an intact UV coating or melamine face.
Plan a clean wood-to-wood bonding area where the joint permits it, or obtain adhesive-manufacturer approval for the exact coated surface and use. A label that says “wood glue” or “melamine glue” does not establish compatibility with every prefinished panel.
Start with a joint map, not a glue brand
Mark the proposed glue area on an offcut. Is it raw face veneer, a freshly cut core edge, an intact clear coating, or a decorative overlay? Identify the mating surface separately. The visible face of the finished cabinet may have little in common with the material exposed inside its joint.
| Surface pair | Practical route to evaluate | What still needs verification |
|---|---|---|
| Raw wood to raw wood | A wood adhesive specified for the material, fit and service conditions | Working time, clamp pressure, cure and joint design |
| Raw plywood edge to intact UV-coated face | Expose a designed raw bonding area, or obtain explicit approval for that coating | A general wood-glue claim does not establish UV-coating compatibility |
| Porous wood-based material to melamine | A documented melamine-to-porous-substrate adhesive, within its stated limitations | Actual laminate, preparation, loading and moisture exposure |
| Finished face to finished face | An adhesive system expressly approved for both nonporous surfaces | Curing route, bondline, coating adhesion and end use |
| Raw edge inside a machined dado | A fitted joint with appropriately prepared bonding surfaces | Actual stock thickness, remaining panel thickness and assembly method |
For the broader material decision, read prefinished versus unfinished plywood for cabinet work. This guide starts after that choice, at the joint itself.
Why scuffing a glossy face is not the same as exposing wood
Light abrasion can change the texture while leaving the coating in place. If the adhesive requires bare wood, a dull-looking surface is not proof that preparation is complete. Conversely, aggressive sanding can damage thin face veneer and leave an uneven joint.
Titebond’s published guidance says its wood glues generally rely on bare wood, and that coating adhesion can limit a bond made over paint or stain. For a UV-coated cabinet panel, the practical next step is to verify that exact coating with the adhesive supplier rather than assume that a familiar wood glue will work.
Where the design permits it, machining a controlled bonding area can preserve the surrounding factory finish. Establish the joint location and remaining material before removing any surface. Do not sand the whole visible face to solve a narrow glue-line problem.
The same distinction matters in preparing prefinished plywood for a new coating: preparation depends on the system you intend to apply, not simply on whether the old face looks shiny.
A dado creates a different bonding surface
A dado can expose raw material in a finished panel while leaving the adjacent face intact. That can create a useful joint location, but it does not supply a universal groove depth or guarantee the strength of the assembly.
Read the actual plywood thickness reference before making a nominal-size tooling assumption. Then check the actual cutter and stock together on a test piece.
Melamine glue is a specific route with specific limits
One manufacturer example is Titebond Melamine Glue. Its documentation lists bonds between porous wood-based substrates and synthetic surfaces such as melamine, vinyl and HPL. It also excludes exterior use, likely moisture exposure, and structural or load-bearing applications.
Those limits matter. Do not present that adhesive as a universal glue for cabinet construction, a wet-area assembly or a loaded shelf joint. Its documented melamine uses also do not establish approval for Berta’s UV-clear-coated birch surface.
Ask the adhesive supplier a concrete question: “Will this product bond this panel’s documented coating to this mating substrate, in this joint, under these loads and conditions?” Include photographs, coating information and the proposed assembly method.
To compare the panel surface families first, use the prefinished plywood collection and the melamine-faced plywood collection. The finish name identifies only part of the assembly.
Two current Berta surfaces that need different checks

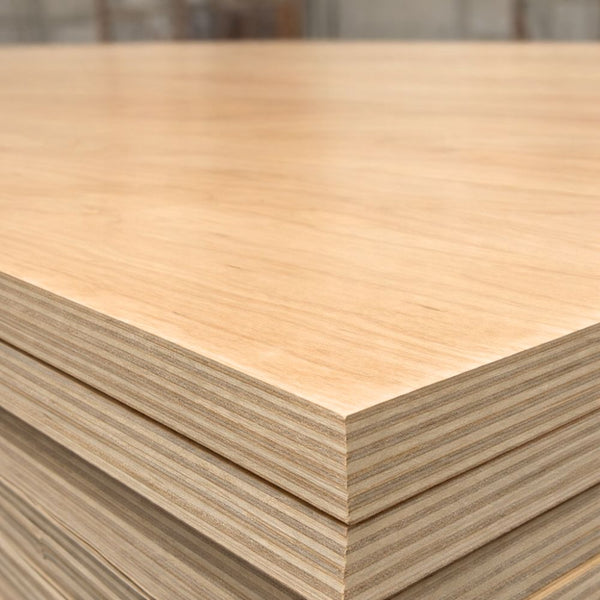
UV-prefinished Birch · 18 mm option
Clear-coated birch veneer over a multi-ply poplar plywood core. Both faces of this selected thickness are factory finished.
Use it for a cabinet interior when you intend to retain that wood surface. Confirm the bonding route for its UV coating, or design prepared raw bonding areas.
Check the Birch panel
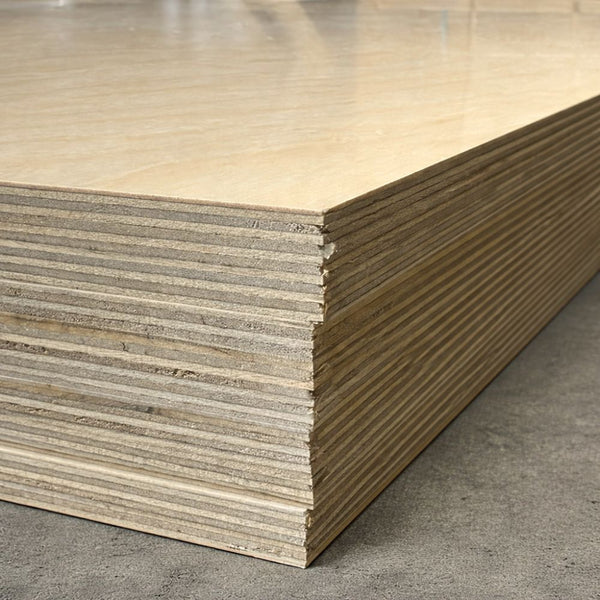
White Melamine · 18 mm option
The standard white melamine option uses a multi-ply poplar plywood core. Both faces of this selected thickness are finished white.
Choose it when a white interior is the intended result. Check any proposed melamine adhesive against its substrate and application limits before assembly.
Check the White Melamine panelEach card uses the current Shopify image for the exact 3/4-inch-class surface shown. These panel descriptions are not adhesive approvals.
Approve an offcut assembly before the cabinet run
Use production offcuts from the actual supplied sheet. A raw scrap from another job does not test the factory coating you will use. If you change the panel, adhesive or preparation, repeat the check.
| Record on the test | Why it matters |
|---|---|
| Panel and face | Identify the exact supplied finish and which surface touches glue |
| Preparation | Record machining, cleaning and any approved abrasion; do not improvise solvents on a decorative finish |
| Adhesive and conditions | Follow its current temperature, working-time and application instructions |
| Joint and clamping | Reproduce the real fit and contact; use pads or cauls that protect visible faces |
| Cure before evaluation | Handling strength is not the same as the manufacturer’s full cure or permission to load |
| Appearance and bond result | Check alignment, squeeze-out marks and separation; an informal test does not create a structural rating |
Protect the visible surface while machining and clamping. Trial the approved cleanup method on an inconspicuous offcut. A solvent or abrasive that removes glue can also damage the finish you paid to keep.
If the assembly uses screws or other mechanical connections, review screw selection for plywood cabinet joints with the actual core, penetration and hardware instructions. Adding screws does not automatically validate an otherwise unsuitable adhesive joint.
Finish the edges as a separate operation
A face-joint adhesive and an edge-banding adhesive do different jobs. Pre-glued veneer, unglued plastic banding and solid edging each need an appropriate application method.
Use the comparison of veneer and PVC edge banding to choose the route, then check the current edge-banding materials. Plan edging thickness and joint dimensions before using the plywood cut-list planner.
For questions about the supplied panel construction, consult the plywood material FAQ or ask Berta Store for the panel specification. Adhesive compatibility should come from the adhesive manufacturer for the actual documented surface.
Questions from the workbench
Can I use ordinary wood glue on UV-prefinished plywood?
Do not assume it will bond reliably to the intact coating. Use an appropriate prepared raw-wood joint or obtain explicit approval for the exact coated surface and application.
Will melamine glue work on clear-coated birch?
A melamine listing does not establish UV-coating compatibility. Treat them as different surfaces and obtain the adhesive supplier’s recommendation.
Should every dado be the same depth?
No. Stock thickness, core, joint geometry and remaining material differ. Establish the depth through the assembly design, then test the fit with the actual panel.
How long should I leave the clamps on?
Use the selected adhesive’s instructions for the actual temperature, material and joint. Distinguish clamp time, handling time and time before loading; do not carry one universal time across adhesive systems.
Source notes and application scope
This is a joint-planning guide for cabinet fabrication. It does not assign a load capacity, adhesive certification or tested glue-system approval to a Berta panel.
- Titebond: bonding over painted or stained surfaces — basis for distinguishing bare wood from an existing coating.
- Titebond Melamine Glue technical information — substrate examples and application limitations, not a Berta product endorsement.
Panel specifications and product-card images were checked against the current Berta Shopify listing on October 7, 2026. Recheck manufacturer instructions when selecting an adhesive.